
A VIMFUN SVI 120-60 endless diamond wire saw. An isostatic graphite block the customer sent us. Two tests on the same machine, same wire, same clamp — slicing, then contour cutting.
Both functions have to pass before the machine ships. That is the whole point of the Factory Acceptance Test. If slicing works but the contour pass drifts, the machine stays in the bay.
The Setup: Factory Acceptance Test Before Shipping
The SVI 120-60 is a vertical endless diamond wire saw built for グラファイトカット. It belongs to the same vertical graphite series as the SVI 80-80, one size up. Vertical layout, closed-loop servo, endless diamond wire loop, dry-cut configuration.
Before any SVI series machine ships, we run a two-function FAT: slicing and contour cutting on the same setup. The reason the FAT exists in that form is that SVI is sold as a multi-function vertical saw. Customers who buy it expect to slice stock in the morning and cut contour parts in the afternoon on the same clamp. If we only tested slicing, we would be shipping half a machine.
For this unit, the customer sent 150 × 150 × 300 mm isostatic graphite blocks from their own stock. They signed off on the parameters first — 180 N tension, 50 m/s wire speed, 80 mm/min feed, Ø 0.8 mm wire, dry. We ran their material at their numbers. Day one on their floor matches what we measured on ours.
Test One: Slicing
Straight-line descent through the full block height. Repeated. We measured thickness on every slice with a digital caliper and spot-checked with a 0–25 mm micrometer. We also looked for chipped edges at entry and exit, wire marks on the face, and kerf width.
| パラメータ | 価値 |
|---|---|
| 加工ワークピース | Isostatic graphite block, 150 × 150 × 300 mm |
| 機械 | VIMFUN SVI 120-60 endless diamond wire saw |
| ワイヤー | Ø 0.8 mm electroplated ダイヤモンドワイヤーループ |
| ワイヤーテンション | 180 N |
| ワイヤースピード | 50 m/s |
| 送り速度 | 80 mm/min |
| 冷却水 | None — dry cutting |
| 粉塵管理 | Negative-pressure extraction at the kerf |
| Kerf width (measured) | ~0.9 mm |
The parameter window comes from our internal reference on ワイヤー速度、張力、送り速度の. 180 N sits in the middle of the 150–200 N band we have validated on isostatic grades. 50 m/s and 80 mm/min are the paired values we already ran on previous isostatic jobs.
Measured result. Every slice came out within ±0.03 mm of nominal across the full slice area. Faces were flat. No visible wire marks under angled light. No chipped edges at entry or exit. Kerf measured 0.9 mm, matching the wire + abrasive diameter.
We sliced 10 pieces off the first block to get a thickness distribution, not just a spot sample. Caliper reading on every slice, logged. The spread stayed inside ±0.03 mm from the first slice to the tenth. Wire tension did not need re-checking between cuts — the loop ran continuous, the tension sensor held 180 N through the full test.
Dry cutting. No coolant. No slurry. No graphite mud. The dust from the kerf went straight into the negative-pressure extraction and ended up in the filter unit as dry powder. No slurry tank to drain, no coolant filter to swap, no parts to degrease before the next step. The graphite powder in the filter is dry and separable — it does not stop being graphite.
Test Two: Contour Cutting
Same clamp. Same wire. Same tension setting. We did not re-fixture, did not swap the wire loop, did not change the tension. The only thing that changed was the toolpath file loaded in the controller.
The toolpath had inside corners, outside radii, and a non-trivial profile — the kind of shape a customer would normally send to a 3-axis CNC. One continuous servo-driven pass. No tool change mid-path, because there is no tool to change: a diamond wire loop runs at constant speed and tension, and the servo axes move the workpiece under it. Straight lines and curves are the same operation at the kerf.
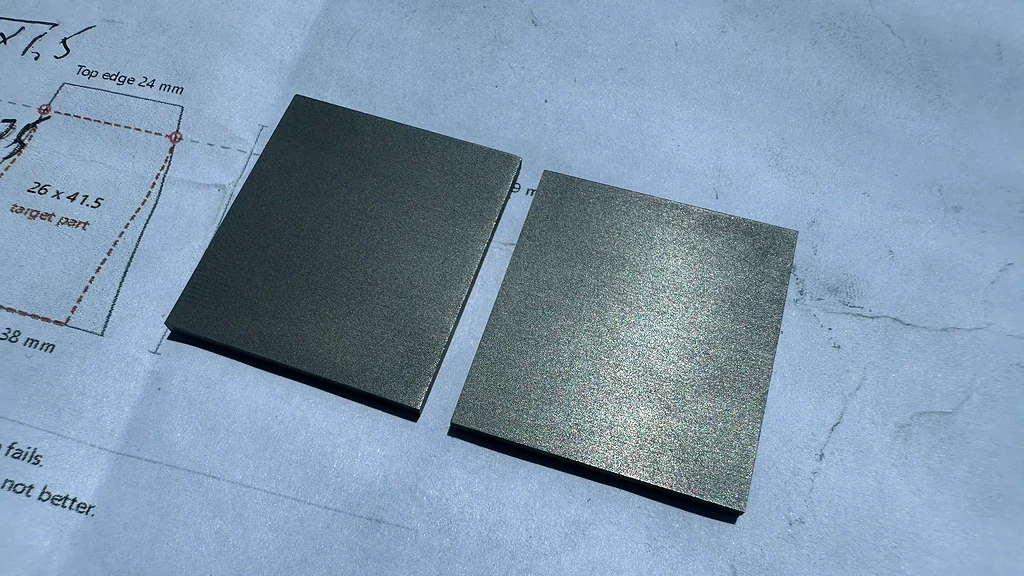
Measured result. Inside corners held the programmed radius. Outside radii came off clean, no step marks between path segments. No witness lines at profile transition points. Edge quality on the contour matched the slicing faces — flat, no fraying, no chipped exits.
We ran the contour toolpath twice on different sides of the same block to check repeatability. Both profiles came off within ±0.03 mm of the programmed path. The wire did not need re-tensioning after Test One, and did not need re-tensioning between the two contour passes.
One side effect worth naming once: the material around the contour comes off the block as a bulk piece with one new machined face. It goes back into stock. Not pulverized to dust.
Pass or Fail: What the Numbers Say
Both tests had to clear the hard thresholds before the FAT sign-off.
| Check | Threshold | Measured |
|---|---|---|
| Slice thickness vs nominal | ±0.03 mm | ±0.03 mm, all slices |
| 切り込み幅 | ≤ 1.0 mm | 0.9 mm |
| Chipped edges at entry/exit | None visible | なし |
| Contour radius vs programmed | ±0.03 mm | Within tolerance |
| Profile transition witness lines | なし | なし |
| Wire condition after FAT | No visible wear bands, no diameter loss > 0.02 mm | Pass |
Diamond wire reference life at 180 N / 50 m/s on isostatic graphite is around 7 days at 8 h/day. The wire from this FAT run went back in the box with plenty of life left — a FAT burns a few hours, not days.
Both functions passed on the first run with the customer’s parameters. FAT sign-off went to the customer with the raw thickness log, kerf measurement, and contour inspection photos.
If You’re Buying This Machine, What You Should Ask For
If you are evaluating the SVI 120-60 for your own isostatic graphite work, the thing to ask for is a FAT on your material, with your parameters, before the machine leaves our floor.
Send us:
- Block size, grade, and supplier
- Target part — a drawing, a sketch, or a photo of a reference part
- Thickness tolerance and the geometry you need (slices, contours, or both)
- Quantity
We run your blocks on the actual machine, measure the results, and send you the thickness log, kerf measurement, and contour inspection photos — plus video of both tests. Only after you sign off does the machine ship.
Compared to the CNC route most shops default to, the saw also keeps the material around the cut as usable stock instead of unrecoverable dust. We cover that trade-off in our writeup on エンドレスダイヤモンドワイヤーソーと従来の方法.
Send us your drawing.







